Choosing industrial automation solutions is not simply a matter of selecting the fastest robot or newest control system. The right choice depends on what your operation must improve, and what it can realistically support. A packaging line, for example, may need steadier output, fewer changeover delays, or better inspection records. Each goal points to different equipment, software, and integration needs. Start with the process, not the product.
Look closely at the work on the factory floor. Note cycle times, unplanned stops, operator tasks, and the conditions around machines, including dust, temperature, and available space. Then check whether proposed systems can communicate with existing controllers, sensors, and production software. Compatibility can be easy to overlook. It can also become expensive later. Ask suppliers for documented performance data, maintenance requirements, training plans, and realistic implementation timelines. A demonstration using your own materials may reveal problems a polished presentation will not.
Safety, scalability, and support matter as much as initial purchase price. Compare total costs over the expected service life, including integration, spare parts, downtime, and staff training. Where possible, test a limited application and define measurable targets before expanding. That is useful. Still, a pilot cannot predict every production issue, and assumptions should be revisited as evidence emerges. Involve operators, maintenance teams, engineers, and qualified integrators in the evaluation. Their practical feedback can expose awkward workflows or service gaps early. A sound decision is rarely perfect; it is transparent about trade-offs and grounded in verified requirements.
Before choosing industrial automation solutions, define the operational result you need. Set measurable goals, such as reducing changeover time from 18 minutes to 12 or lowering rejected parts per shift. Be specific. A packaging line may need steadier output during peak hours, while a machine shop may need fewer manual measurements between operations. Separate must-have outcomes from nice-to-have improvements.
Then draw a clear boundary around the work. Identify which machines, tasks, and data flows belong in the project, and which should remain unchanged. Map the current process on the floor, including operator handoffs, material queues, and awkward pauses that rarely appear in official cycle times. Record a normal shift, not just an ideal run. The baseline can be messy. Set practical limits for downtime, staffing, floor space, and maintenance skills. Include operators and technicians in these discussions; they often know where small jams repeatedly form. A pilot on one cell can test assumptions before wider deployment, but it may not capture every shift pattern. Keep room to revise the scope when measured results differ from expectations.
Define the operational goals and automation scope before selecting equipment or software.
Example planning targets relative to a site's current baseline: increase throughput by 15%, reduce cycle time by 20%, unplanned downtime by 25%, defect rate by 30%, and changeover time by 40%. Measure the baseline first and adjust targets to fit the process.
Start at the production line, not with a machine catalog. Follow one product through each operation and record cycle time, changeover duration, defect rate, and unplanned stops. Watch a real shift. A process map may miss the operator’s brief pause to clear a jam or adjust a fixture. These small interruptions can shape the actual capacity requirement. Identify the bottleneck before specifying automation; speeding up a non-bottleneck station may only create a larger queue downstream.
Technical fit matters as much as speed. Check part variation, payload, reach, accuracy, available floor space, and how equipment will exchange data with existing controls. Also assess guarding, maintenance access, and staff training needs. The International Federation of Robotics reported 541,302 industrial robot installations worldwide in 2023 in its World Robotics 2024 report. That scale shows how widely automation is being adopted, but it does not make every process a good candidate. Still, measurements can be misleading. Recheck them across different shifts and product mixes.
Choosing industrial automation solutions starts with comparing how each technology fits the process. A programmable controller may suit predictable machine sequences, while an industrial computer can handle heavier data tasks. Motion controllers need to match motor feedback, cycle times, and positioning accuracy. Check communication protocols, available ports, and signal types before selecting equipment. A sensor with the wrong output can turn a simple installation into extra wiring and troubleshooting.
Tips: Map existing devices and list their protocols, voltage ranges, and connection points. Test a representative sensor and controller together before ordering for the whole line. Check response time under realistic operating conditions, not just in a quiet test setup. Keep the results.
Compatibility also depends on the site. Dust, vibration, temperature, and cabinet space affect hardware choices. Confirm that software versions can exchange data with existing systems, and ask who will maintain the configuration. A compatibility spreadsheet can look complete and still miss an older device tucked inside a control cabinet. We have seen small details like that delay commissioning. Reserve time for a physical inspection, and document any assumptions. If future expansion matters, check spare ports and processing capacity now; replacing a controller later may cost more than expected.
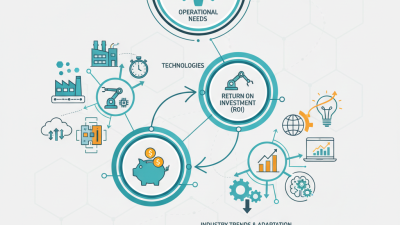
When evaluating industrial automation suppliers, look beyond a polished demonstration. Ask for references from facilities with similar production volumes and operating conditions. Check whether the supplier can explain system limits, integration requirements, and commissioning responsibilities in plain language. Request a site visit or a sample test using your own parts. Small details matter.
Compare the full cost of ownership, not just the purchase price. Include installation, operator training, software updates, spare parts, and planned maintenance. Ask what happens when a critical component fails at 2 a.m. A low initial quote may leave expensive gaps. Put service response times, remote support, and parts availability in writing. Cost estimates are rarely perfect, so leave room for unexpected integration work.
Safety deserves a practical review before equipment is selected. Identify pinch points, emergency stops, access doors, and tasks that require people to work near moving machinery. Ask how the proposed safeguards will be tested and maintained. Operators should be involved; they often notice awkward access or unclear alarms that a drawing misses. Training should include realistic fault scenarios, not just routine startup. No system is risk-free. Revisit the assessment after installation, especially when workflows or production rates change.
| Solution Type | Typical Applications | Supplier Evaluation Checks | Relative Upfront Cost | Safety Considerations | Support and Lifecycle Checks | Best-Fit Indicators |
|---|---|---|---|---|---|---|
| PLC-based control | Discrete machines, packaging lines, conveyors, and equipment with defined sequences. | Confirm experience with the required I/O, motion, communications, environmental conditions, and machine cycle times. Request project references for comparable applications. | Low to medium for a standalone machine; increases with I/O count, motion control, integration, and commissioning scope. | Use appropriately rated safety components for safety functions. A standard PLC is not a substitute for a safety-rated control system. | Check spare-parts availability, backup and restore procedures, software access, documentation, and response times for troubleshooting. | The process is machine-focused and can be controlled with clear, localized logic. |
| PAC-based control | Complex machines or coordinated production systems requiring larger programs, data handling, motion, or multiple communication networks. | Verify system capacity, supported protocols, network diagnostics, programming skills, and ability to integrate with existing equipment and supervisory systems. | Medium; total cost depends on system size, integration effort, and the level of motion or data functionality required. | Define safety functions separately and confirm that the proposed safety hardware and design meet the project risk assessment. | Assess engineering-tool licensing, training, long-term availability, upgrade paths, and the supplier’s ability to support the installed configuration. | Several machine functions must be coordinated, or advanced control and data handling are needed. |
| DCS (Distributed Control System) | Continuous or batch processes such as chemical, water treatment, power, and other process operations. | Review process-industry experience, redundancy design, alarm management, controller capacity, integration approach, and migration plan for existing controls. | High; typically reflects system engineering, operator interfaces, process integration, redundancy, testing, and commissioning. | Separate process safety requirements from basic process control. Determine required safety instrumented functions through a formal risk assessment. | Confirm 24/7 support availability if needed, lifecycle services, patching practices, backup arrangements, and support for planned system upgrades. | Many process variables and operating units need coordinated control and centralized operator oversight. |
| SCADA and supervisory monitoring | Monitoring and supervisory control across plants, utilities, remote sites, or geographically distributed assets. | Check data acquisition capacity, historian requirements, alarm handling, remote connectivity, user access controls, and interoperability with existing control systems. | Low to high depending on the number of sites, data points, communications infrastructure, software scope, and cybersecurity requirements. | Keep critical protective functions in suitable local control or safety systems. Apply secure remote-access controls and role-based permissions. | Review software updates, backup and recovery, cybersecurity maintenance, operator training, and support for connected field devices. | Operators need a shared view of status, alarms, trends, and supervisory commands across multiple assets. |
| Safety PLC or safety-rated control system | Safety-related machine or process functions, such as emergency stops, interlocks, and monitored access protection. | Ask for evidence of suitable safety-system capability, documented validation methods, competent functional-safety personnel, and traceable design records. | Medium to high; depends on the number and complexity of safety functions, required integrity, and validation effort. | Base the design on a documented risk assessment and applicable standards, such as ISO 13849-1 or IEC 62061 for machinery. Validate the completed safety functions. | Require change-control records, validation documentation, periodic review arrangements, and access to qualified support for modifications. | Risk assessment identifies safety functions that require safety-rated logic and components. |
| Industrial robot or robotic cell | Pick-and-place, machine tending, palletizing, welding, and repetitive handling tasks. | Evaluate application experience, payload and reach suitability, cycle-time evidence, integration capability, simulation process, and operator training. | Medium to high; tooling, guarding, safety equipment, integration, and commissioning can be substantial parts of the project cost. | Assess the complete cell, including robot, tooling, access points, and operating modes. Select safeguards based on a risk assessment and validate them before use. | Check maintenance training, spare tooling and components, recovery procedures, backup files, and availability of qualified service technicians. | The task is repetitive and can be performed within a defined work envelope with suitable safeguarding. |
| Industrial networking and edge data systems | Connecting controls, collecting production data, and supporting condition monitoring or analytics. | Confirm protocol compatibility, data ownership, network segmentation, time synchronization, device capacity, and integration with plant systems. | Low to medium for a limited data-collection deployment; rises with plant-wide connectivity, sensors, and cybersecurity controls. | Do not let analytics or data systems bypass established control and safety functions. Assess remote access and network-security risks. | Clarify software maintenance, data retention, backup, security updates, and support responsibilities across system interfaces. | Reliable production data or connectivity is needed without replacing the existing control architecture. |
Cost guide: Relative cost levels are planning indicators, not quotations. Actual project costs depend on scope, site conditions, integration, downtime, engineering, commissioning, training, and lifecycle requirements. Compare suppliers using the same written scope and evaluate total cost of ownership, not purchase price alone.
Plan industrial automation around the work it must improve, not a technology list. Map one production line, including manual handoffs, changeovers, and downtime. Set a baseline for cycle time, defects, and unplanned stops before installing equipment. Then run a contained pilot with operators and maintenance staff involved. A tidy pilot can hide messy realities, so test unusual shifts and product changes too.
Integration needs equal attention. Check how proposed controls will exchange data with existing machines, production software, and quality systems. Define data ownership, network access, and failure procedures before commissioning. The International Federation of Robotics’ World Robotics 2024 report counted more than 4.28 million industrial robots operating worldwide in 2023, a 10% rise from 2022. That scale makes workforce training and maintainable designs practical priorities, not optional extras. Leave space in control cabinets, document interfaces, and select modular equipment that can support another cell or sensor later.
Tips: Start with one measurable bottleneck. Record baseline results. Involve technicians early. Keep a manual fallback, and review the pilot after several production cycles; early results can flatter a system.
Arsun Engineers is the well-known manufacturer, exporter, and supplier of highly operational machines.